Heat Exchanger Tube That Holds Its Duty
Fanbang makes the bare tube, bonds the fin to it and drills the tubesheet that holds it - eight fin geometries, three alloy families, one works in Jiangsu supplying heat exchanger and boiler builders in more than 20 countries.
- 12+Years Manufacturing
- 20+Export Countries
- 8Fin Geometries
- 25Tube Mill Machines
Four Product Families Built Around One Bundle
A heat exchanger needs a tube that resists the process, a fin that moves the heat and a plate that holds both. We produce all three, which is why the hole pattern matches the tube when the crates are opened.
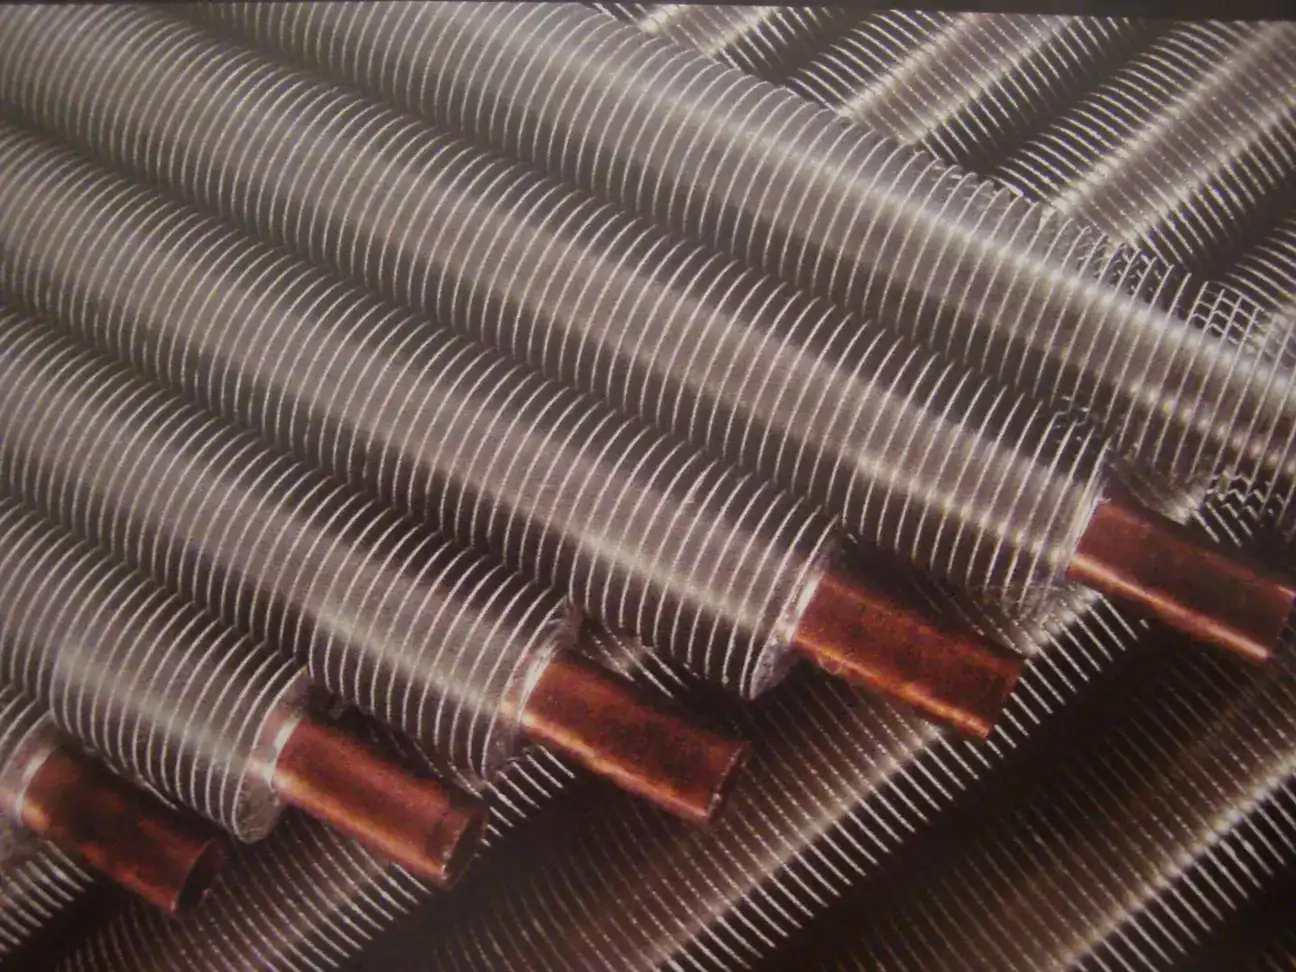
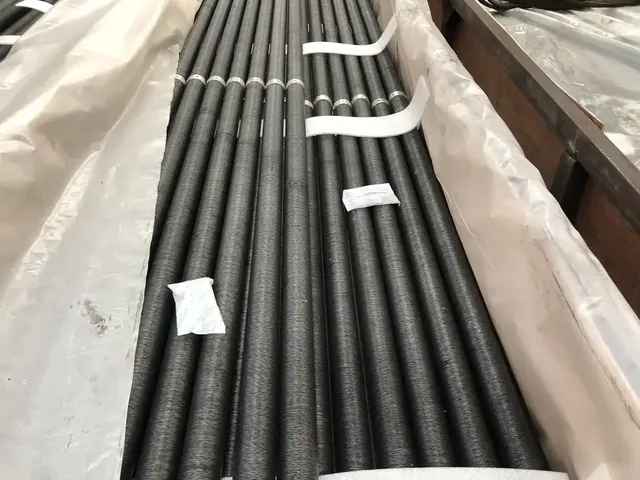 Mechanical Finned TubeFins bonded to the tube by groove, tension or extrusion - the air cooled heat exchanger familyView Mechanical Finned Tube
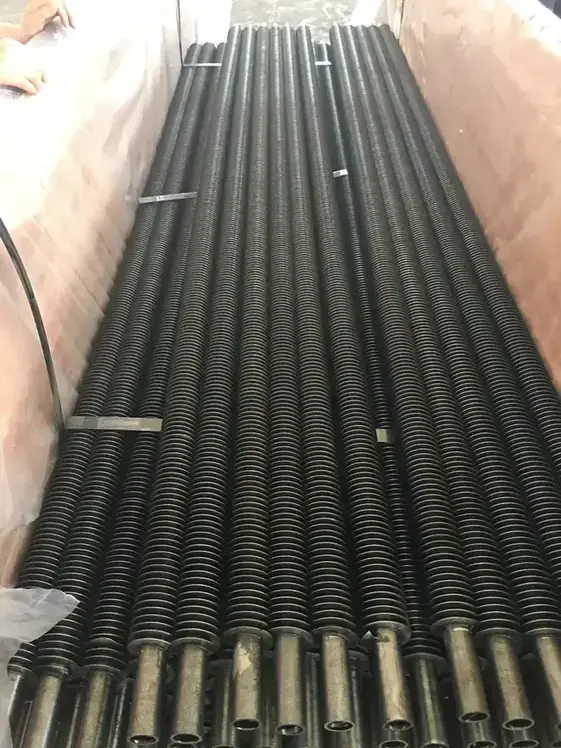 Welded Finned TubeSpiral, H type, longitudinal and stud fins welded to the tube for flue gas serviceView Welded Finned Tube
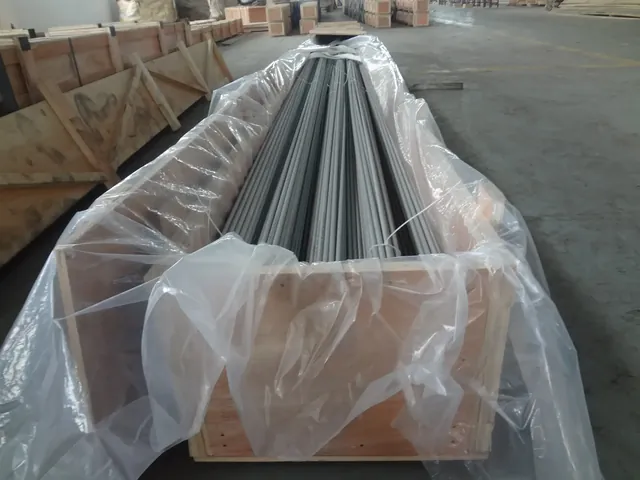 Seamless TubeStainless, duplex and nickel alloy seamless tube and pipe from our own 25 machine workshopView Seamless Tube
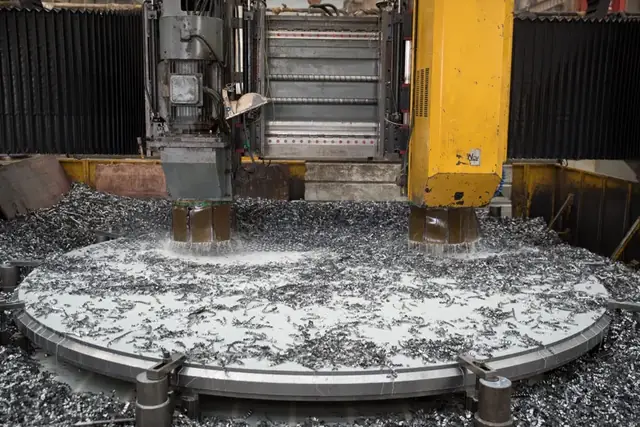 TubesheetsDrilled tube plate to 5000 mm diameter, matched to the bundle we supplyView Tubesheets
Every Tube We Produce
Twelve products across mechanical fins, welded fins, seamless tube and tubesheets. Dimensions on each page are the ranges our lines actually run.
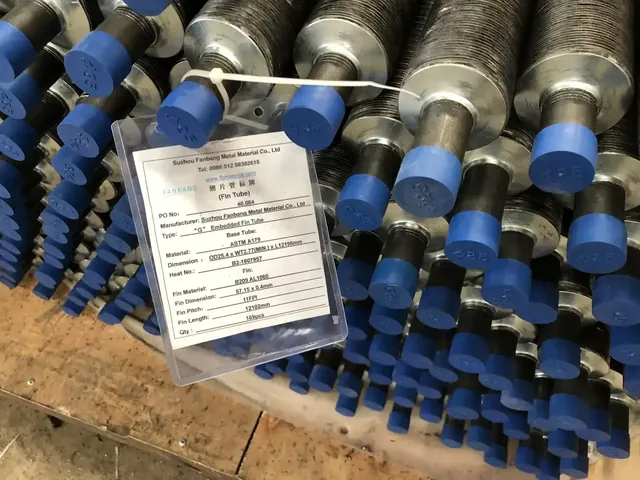 "G" Embedded Fin Tube
Fin strip rolled into a machined groove in the tube wall for permanent metal-to-metal contact
Base tube diameter: 16 mm - 80 mm · Base tube wall thickness: 1.65 mm - 4.0 mm
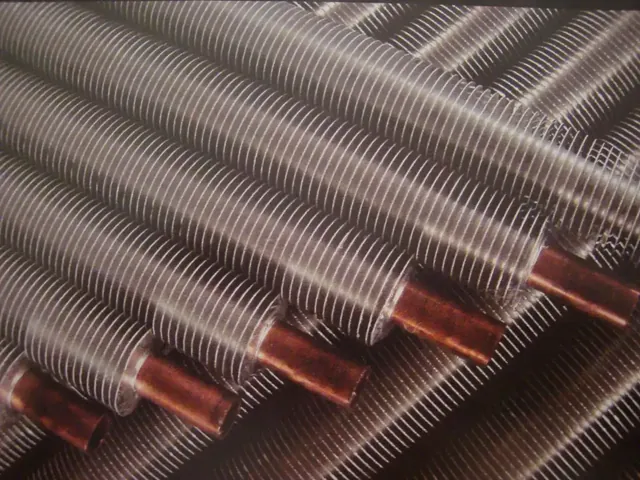 L/LL/KL Fin Tube
Tension-wound foot fin in three footprint styles, the standard choice for air cooled heat exchangers
Base tube diameter: 19 mm - 51 mm · Base tube wall thickness: 1.65 mm - 3.0 mm
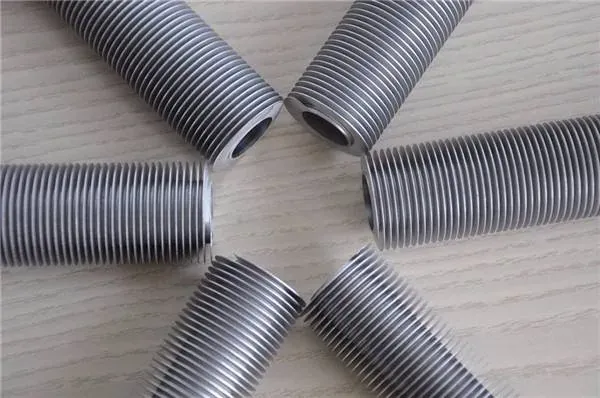 Extruded Fin Tube
Bimetal tube with the fin extruded from an outer sleeve, giving a seamless fin-to-tube wall
Base tube diameter: 10 mm - 51 mm · Base tube wall thickness: 1.65 mm - 3.0 mm
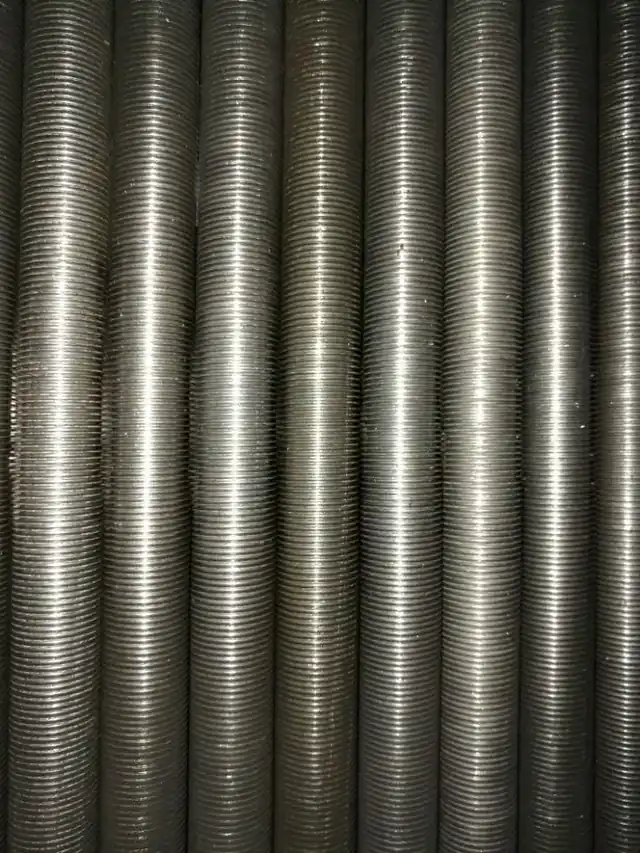 Low Fin Tube
Integral low fin rolled from the tube wall itself, for shell and tube exchangers
Base tube diameter: 12.7 mm - 31.8 mm · Base tube wall thickness: 1.65 mm - 3.0 mm
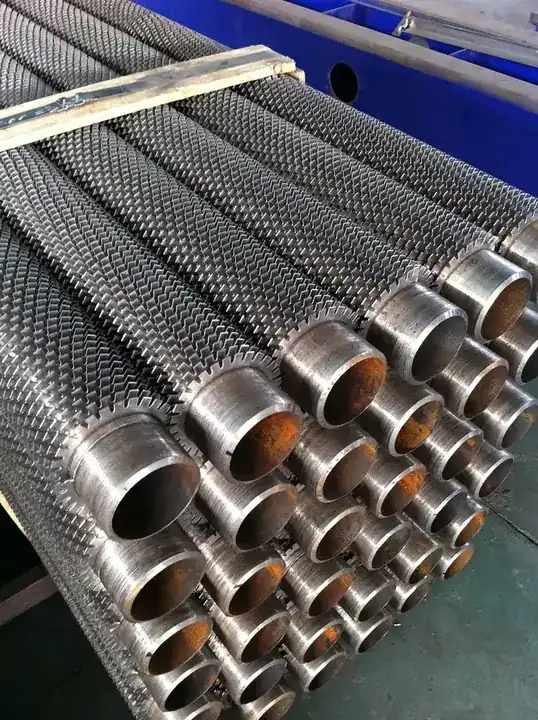 Spiral Fin Tube
Continuously welded helical fin for boiler, economizer and flue gas duty
Base tube diameter: 15 mm - 70 mm · Base tube wall thickness: 2.0 mm - 15.0 mm
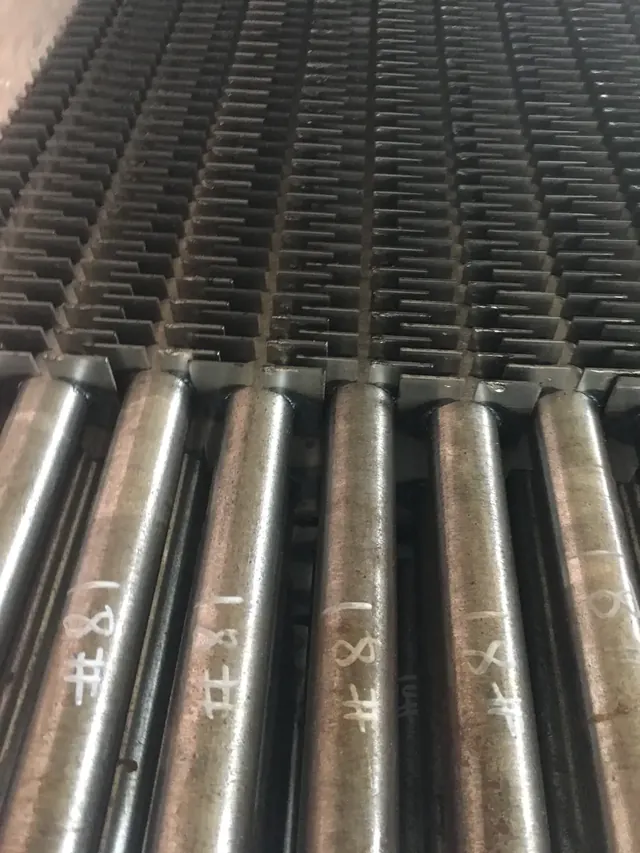 H/HH Fin Tube
Split square fins welded in pairs, leaving a straight ash lane along the tube
Base tube diameter: 25 mm - 73 mm · Base tube wall thickness: 3.0 mm - 6.0 mm
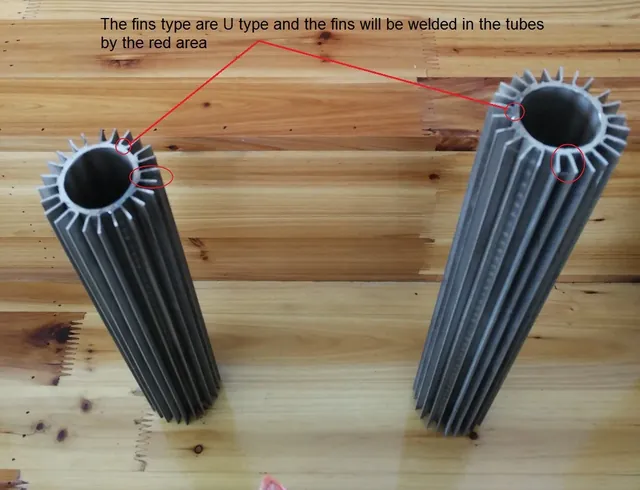 Longitudinal Fin Tube
Straight fins welded along the tube axis for viscous fluids and low velocity gas
Base tube diameter: 12 mm - 273 mm · Base tube wall thickness: 2.11 mm - 25.4 mm
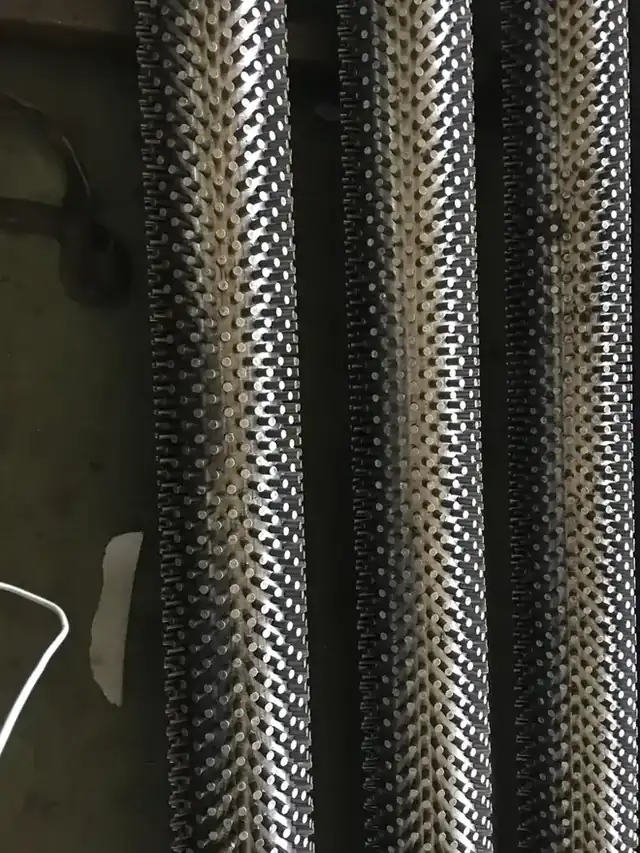 Stud Fin Tube
Individually welded studs for the dirtiest furnace and process heater duty
Base tube diameter: 38 mm - 273 mm · Base tube wall thickness: 3.5 mm - 10.0 mm
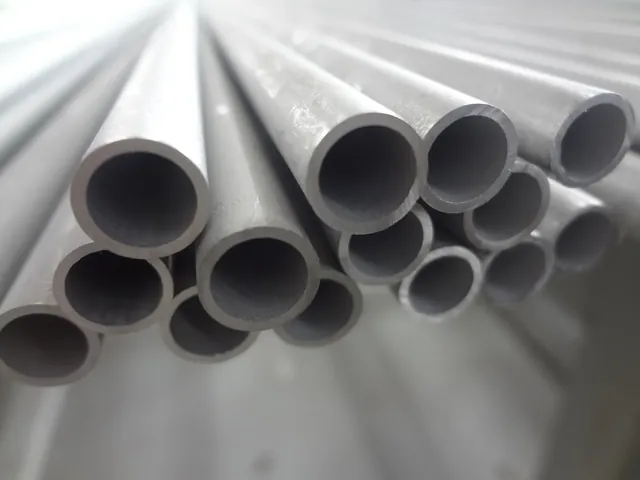 Stainless Steel Tube
Austenitic and super austenitic seamless tube and pipe to ASTM A213, A269 and A312
Tube outside diameter: 1/2" - 3" (12 mm - 76.2 mm) · Tube wall thickness: 0.02" - 0.5" (0.5 mm - 12.0 mm)
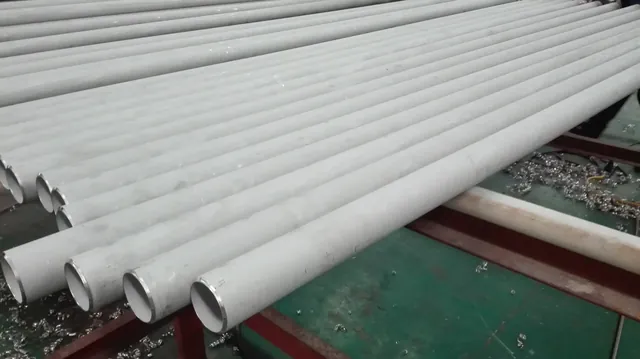 Duplex Stainless Steel Tube
Duplex and super duplex seamless tube and pipe to ASTM A789 and A790
Tube outside diameter: 1/2" - 3" (12 mm - 76.2 mm) · Tube wall thickness: 0.02" - 0.5" (0.5 mm - 12.0 mm)
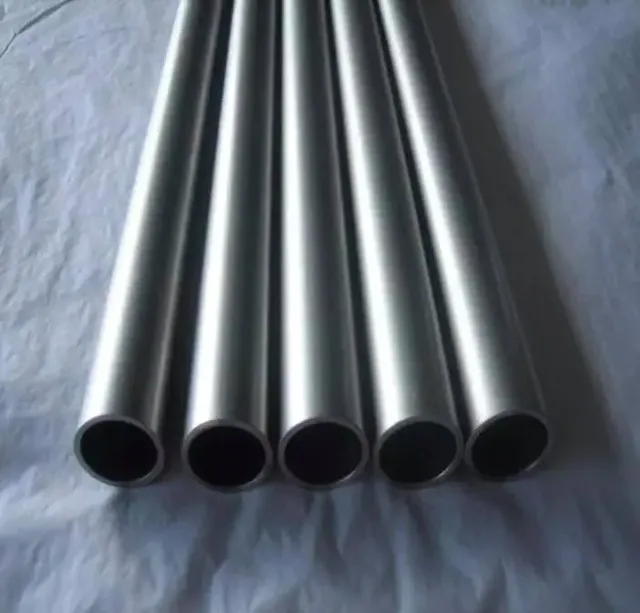 Nickel / Nickel Alloy Tube
Monel, Inconel, Incoloy and Hastelloy grade seamless tube for the hardest corrosion duty
Tube outside diameter: 1/2" - 3" (12 mm - 76.2 mm) · Tube wall thickness: 0.02" - 0.5" (0.5 mm - 12.0 mm)
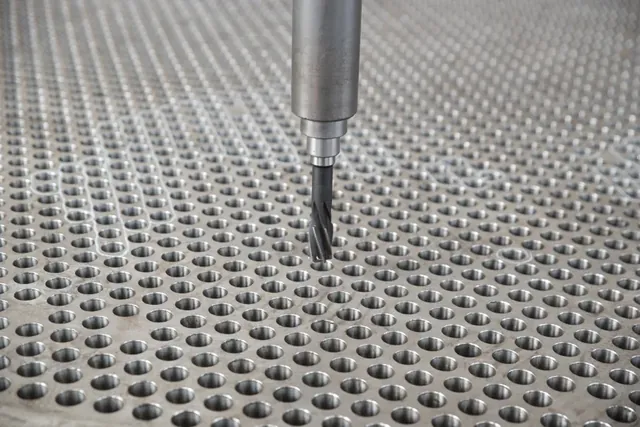 Tubesheet
Drilled tube plate up to 5000 mm diameter and 750 mm thick
Maximum outside diameter: 5000 mm · Maximum thickness: 750 mm
Bundles Fail at the Fin Before They Fail at the Tube
Three things end a heat exchanger bundle's service life, and the fix for each is a different bond, not a bigger bundle.
Fins loosening under heat
A tension wound fin relies on contact pressure. Once metal temperature relaxes it, contact resistance rises and the calculated duty disappears. Embedded and welded bonds are the answer.
Corrosion under the fin foot
Where the atmosphere reaches the exposed base tube, corrosion works underneath the fin where nobody inspects. Extruded tubes cover the parent metal along the whole finned length.
Ash and slag blinding the bank
Continuous fins bridge over with deposits until gas side pressure drop forces an outage. H type fins leave an ash lane; stud fins leave gaps in every direction.
Industries We Supply
Heat exchanger and boiler builders, EPC contractors and plant operators across the European, American and Gulf markets.
Power Generation
Power plants buy tube for two jobs: recovering heat that would otherwise leave through the stack, and rejecting heat that has already done its work. B...
Petrochemical and Refining
Refinery heat transfer equipment fails in two ways: the fire side fouls and the process side corrodes. Fanbang supplies both sides of that problem - w...
Oil and Gas Processing
Gas treatment and oil processing plants sit in the worst atmospheres their own product creates - salt air, sour gas, heavy residues. Tube choice here ...
HVAC and Refrigeration
Refrigeration and climate control bundles are built to a fixed envelope and a fixed price. The tube has to add surface without adding size, and keep d...
Food and Pharmaceutical
Food and pharmaceutical plant work to a different constraint from process industry: surfaces have to be cleanable and the material has to be traceable...
Two Workshops Under One Company
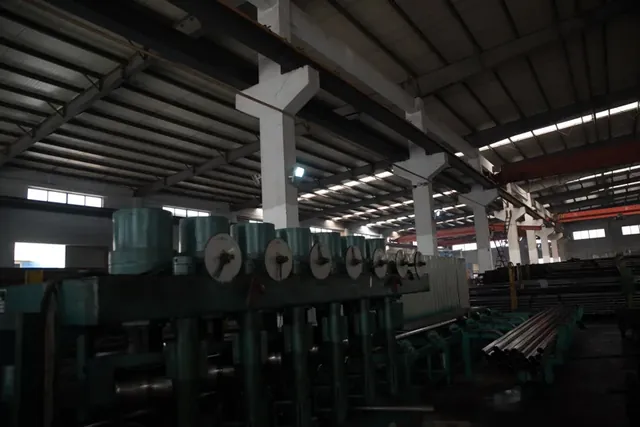
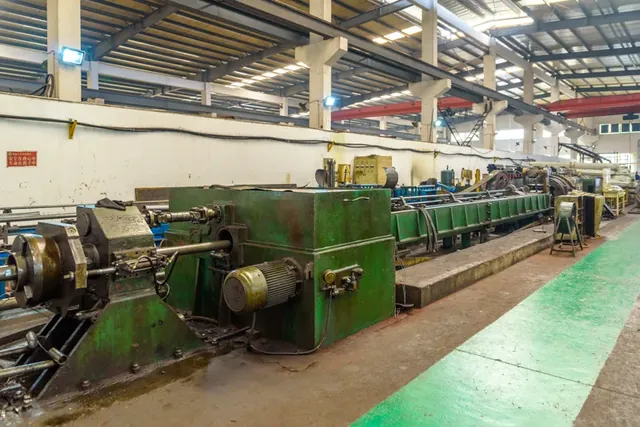
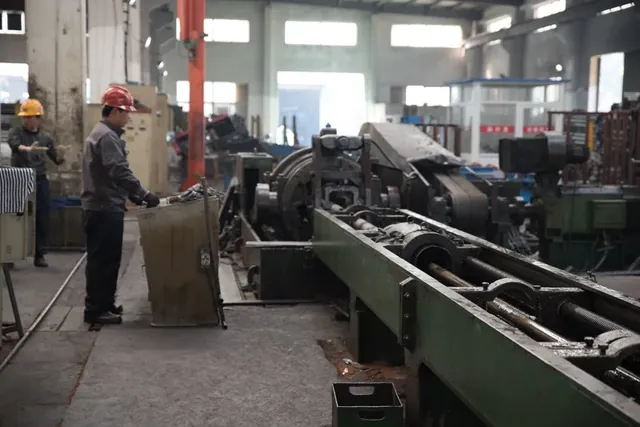
A seamless tube workshop with 25 rolling and cold drawing machines, and a fin tube workshop running 23 machines and lines across the eight geometries.
How Buyers Work With Us
Heat Exchanger Bundle Supply
Buying a bundle's parts from three suppliers means three interpretations of one drawing. This is the route where tube, fin and tube plate come from the same document and the same works.
Boiler and Heat Recovery Surface
Economizer surface is chosen by what the flue gas carries, not by what the duty calculation alone suggests. Four geometries cover the range from clean gas to slagging furnace duty.
Corrosion Resistant Tube Selection
Most tube failures we are asked to replace were grade selection decisions, not manufacturing defects. This is the sequence we work through with a buyer before a grade is fixed.
Tested on Our Own Equipment Before It Ships
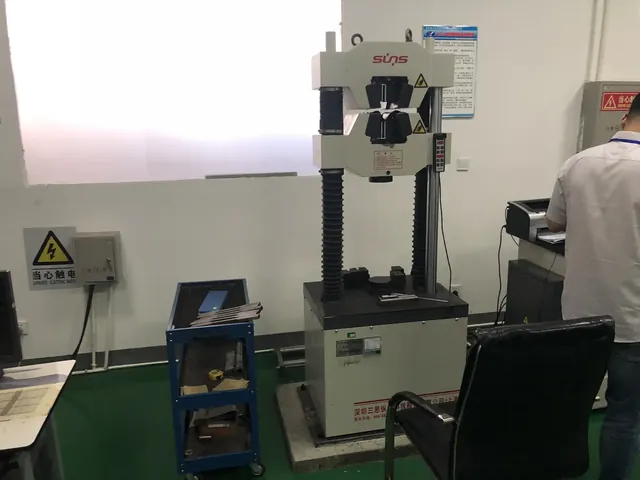
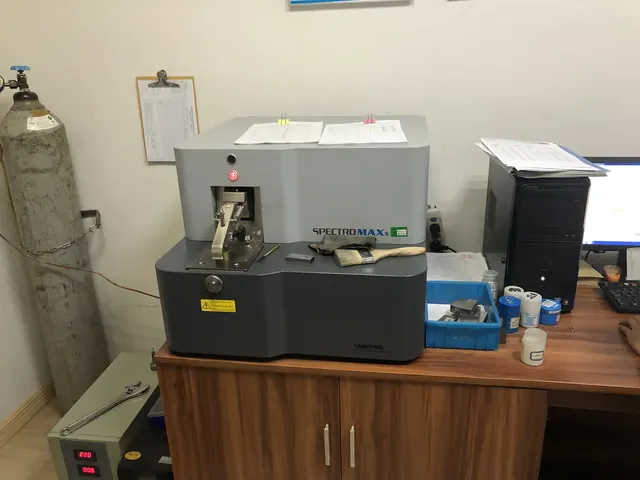
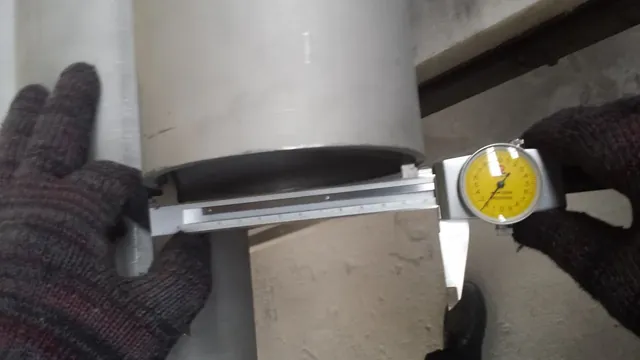
Eddy current, hydro test, tensile, flattening, flaring, hardness, chemical analysis and dimensional inspection - carried out in house, with raw material from established suppliers including Yongxing steel.
- Eddy current
- Hydro test
- Tensile testing
- Flattening testing
- Flaring testing
- Hardness testing
- Chemical testing
- Dimension inspection
Guides From Our Engineering Desk
 Fin Tube Types Explained and How to Choose OneL type, embedded, extruded, low fin, spiral, H type, longitudinal and stud fins compared by bond, temperature limit and ...
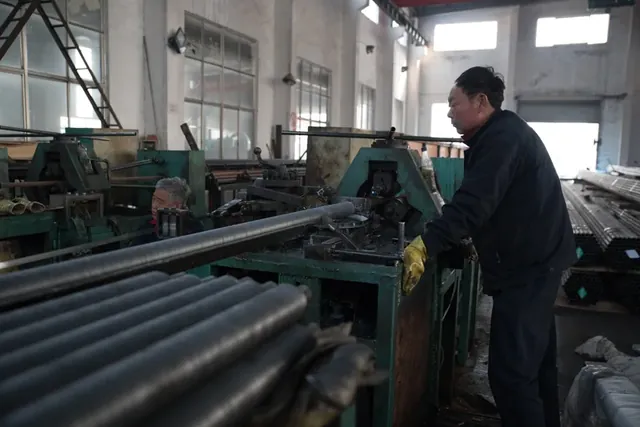 Embedded vs Extruded Fin Tube for Air Cooled Heat ExchangersA direct comparison of G type embedded and extruded bimetal fin tube: bond mechanism, base tube range, atmospheric prote...
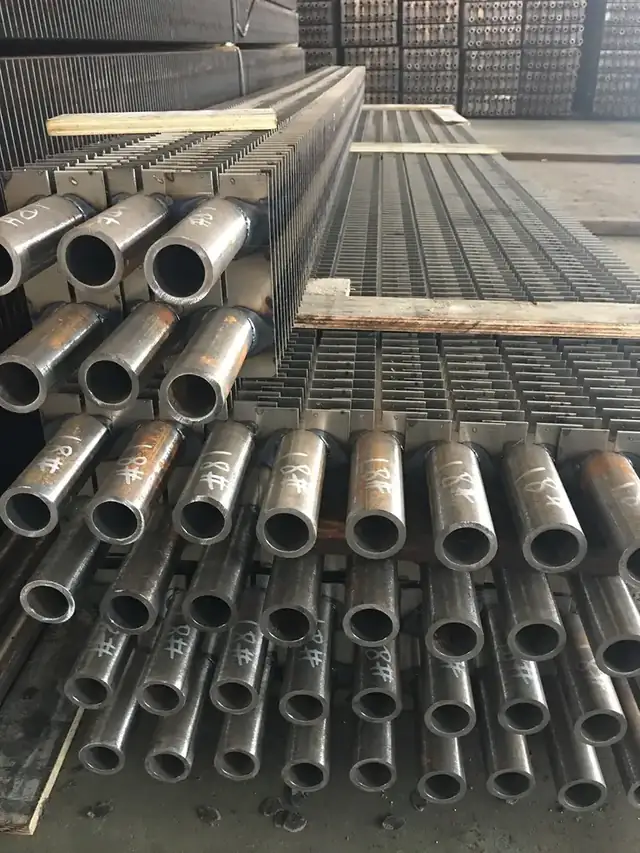 Why H Type Fin Tube Survives Ash Laden Flue GasHow the split fin geometry of H and HH type finned tube keeps economizer banks cleanable, with fin pitch, fin thickness ...
Questions Buyers Ask Before the First Order
Do you make the bare tube as well as the fin?
Yes. The seamless tube workshop runs 25 rolling and cold drawing machines, and the fin tube workshop runs 23 machines and production lines. The bare tube and the finned tube come from the same company.
Which fin geometries can you produce?
Eight: G type embedded, L/LL/KL tension wound, extruded, integral low fin, spiral welded, H and HH, longitudinal and stud.
What base tube sizes do you cover?
From 10 mm outside diameter on extruded fin tube up to 273 mm on longitudinal and stud fin tube, with walls from 0.5 mm to 25.4 mm depending on the product.
Which certificates do you hold?
ISO 9001:2015, a CE certificate and a production licence for pressure pipe.
Which markets do you export to?
More than 20 countries, with most experience in the European, American and Gulf markets.
How do I get a quotation?
Email [email protected] with the bundle drawing or the tube schedule. Quotations are issued against the drawing, and we tell you what data is missing rather than assuming it.
Send Us the Bundle Drawing
Tube size, fin geometry, alloy and tubesheet layout - we quote against the drawing and tell you where the specification and the layout disagree.
[email protected] · Tel 0086 512 58392615 · Monday to Saturday, 08:30 - 17:30 China Standard Time (GMT+8)