Slitting, Edge Conditioning and Tolerance
Width to the coil dimension, edges rounded, no burrs and no scratches - because the burr is what causes the turn-to-turn fault three weeks after delivery.
Why the edge decides the coil
Every roll is checked so that it carries no burrs and no scratches and has a round edge suited to transformer winding. That is not cosmetic. A burr on a foil edge cuts the interlayer film as the coil is wound under tension, and the resulting fault typically appears at test, after the coil is already impregnated.
Slit to your width, not to stock
Aluminium is slit from 20 to 1500 mm and copper from 50 to 1350 mm, so the material arrives at coil width. Nothing is trimmed on the winder and the offcut does not become your scrap.
Dimensional tolerance
Width, thickness and length are held to tolerance limits determined by the transformer design requirement and the applicable industry standard, agreed before the order runs rather than argued after delivery.
Equipment behind it
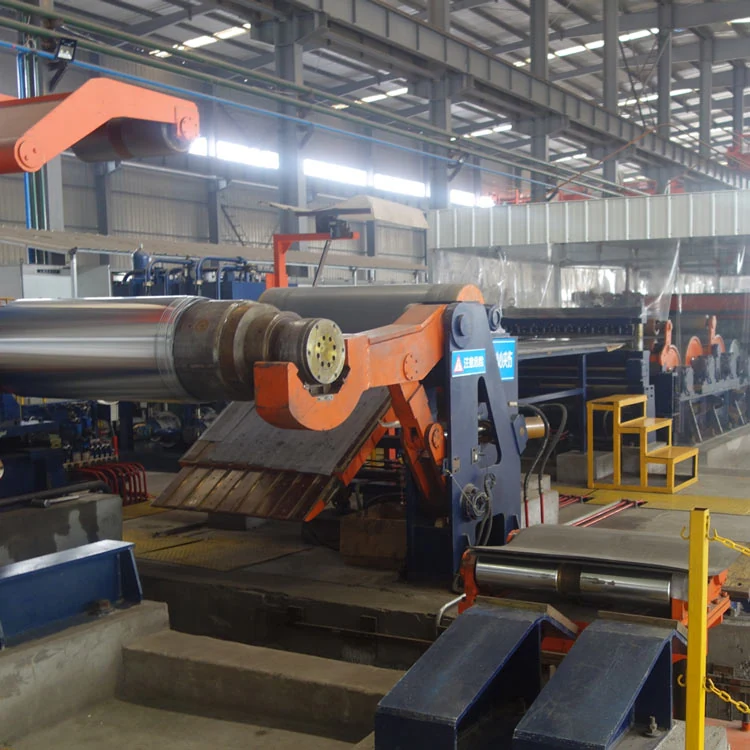
The factory operates a complete set of equipment covering cold rolling, hot rolling, cutting and trimming, built up over more than twenty years of supplying power equipment customers.
Have a dimension you cannot source?
Narrow widths, odd inner diameters and single coils are all quotable. There is no minimum order quantity.